Introduction to Vacuum Systems
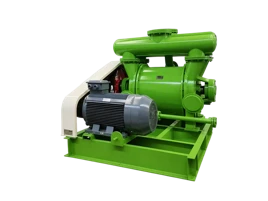
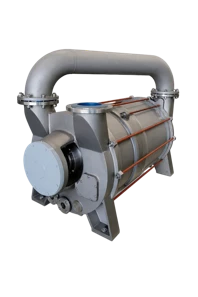
A vacuum system is a crucial component in various industries, designed to create and maintain a pressure lower than the ambient atmospheric pressure. These systems play a vital role in a wide range of applications, including semiconductor manufacturing, food packaging, chemical processing, and scientific research. By removing gas molecules from a sealed volume, vacuum systems enable processes that require a controlled environment, such as thin - film deposition, vacuum drying, and electron microscopy. The performance of a vacuum system is determined by factors like pumping speed, ultimate pressure, and reliability. Different types of vacuum pumps, such as rotary vane pumps, turbomolecular pumps, and diffusion pumps, are used in combination to achieve the desired vacuum level.
Top 10 Vacuum System Manufacturers
1. Shandong Boke Vacuum Technology Co., Ltd.
Shandong Boke Vacuum Technology Co., Ltd. is a leading Chinese manufacturer in the vacuum system industry. The company has a state - of - the - art R & D center and production facilities, enabling it to develop and produce high - quality vacuum products. With a team of experienced engineers and technicians, Shandong Boke is committed to innovation and continuous improvement.
Features in Vacuum System
- Diverse Product Range: Shandong Boke offers a comprehensive range of vacuum pumps and systems, including oil - sealed rotary vane pumps, dry screw vacuum pumps, and vacuum systems for specific applications. This diversity allows customers to find the most suitable solution for their needs.
- High - Quality Materials: The company uses high - quality materials in the manufacturing process, ensuring the durability and reliability of its products. For example, in its dry screw vacuum pumps, the screws are made of special alloys that can withstand high - temperature and high - pressure environments, resulting in longer service life.
- Energy Efficiency: Shandong Boke's vacuum systems are designed with energy - saving features. Their advanced control systems can adjust the pumping speed according to the actual requirements of the process, reducing energy consumption and operating costs.
Company Advantages
- Customization Capability: Shandong Boke can customize vacuum systems according to the specific needs of customers. Whether it is a small - scale laboratory application or a large - scale industrial production line, the company can design and manufacture a tailored solution.
- After - sales Service: The company provides excellent after - sales service, including installation, commissioning, maintenance, and repair. Their service team is available 24/7 to respond to customer inquiries and solve problems promptly.
- Competitive Pricing: Compared with some international competitors, Shandong Boke offers high - quality products at a more competitive price. This makes its products more accessible to a wider range of customers, especially small and medium - sized enterprises.
Website: https://www.bokevac.com/
2. Edwards Vacuum
Edwards Vacuum is a well - known global player in the vacuum technology field. With a history dating back over a century, the company has established a strong reputation for its innovative products and reliable performance.
Features in Vacuum System
- Advanced Pumping Technology: Edwards offers a wide range of pumping technologies, such as turbomolecular pumps, cryogenic pumps, and scroll pumps. Their turbomolecular pumps are known for their high pumping speed and low vibration, making them ideal for applications in the semiconductor and thin - film industries.
- Integrated Solutions: The company provides integrated vacuum solutions that combine multiple pumps and control systems. This ensures seamless operation and optimal performance in complex industrial processes. For example, in the semiconductor manufacturing process, Edwards' integrated systems can precisely control the vacuum environment to meet the strict requirements of chip production.
- Environmental Friendliness: Edwards is committed to developing environmentally friendly vacuum products. Their dry pumps eliminate the need for oil, reducing the risk of oil contamination and minimizing the environmental impact.
Company Advantages
- Global Presence: Edwards has a vast global network of sales and service centers, which allows it to provide timely support to customers around the world. This global reach ensures that customers can access technical assistance and spare parts quickly.
- Research and Development: The company invests heavily in research and development to stay at the forefront of vacuum technology. Their R & D efforts focus on improving product performance, energy efficiency, and reliability.
- Industry Experience: With over 100 years of experience in the vacuum industry, Edwards has in - depth knowledge of various applications and customer requirements. This experience enables them to provide customized solutions and expert advice.
3. Pfeiffer Vacuum
Pfeiffer Vacuum is a German company that has been a pioneer in vacuum technology for many years. It is known for its high - precision vacuum measurement and control systems.
Features in Vacuum System
- Accurate Vacuum Measurement: Pfeiffer Vacuum's vacuum gauges are renowned for their high accuracy and reliability. They can measure vacuum levels from atmospheric pressure down to ultra - high vacuum, providing precise data for process control.
- Smart Control Systems: The company's control systems are equipped with advanced software that allows for real - time monitoring and adjustment of the vacuum system. This smart control ensures stable and efficient operation of the system.
- Modular Design: Pfeiffer Vacuum's products have a modular design, which makes them easy to install, maintain, and upgrade. Customers can add or remove components according to their changing needs.
Company Advantages
- Quality and Precision: German engineering is synonymous with quality and precision, and Pfeiffer Vacuum lives up to this reputation. Their products are manufactured to the highest standards, ensuring long - term performance and reliability.
- Application Expertise: Pfeiffer Vacuum has extensive application expertise in various industries, such as analytics, coating, and vacuum furnaces. They can provide tailored solutions based on the specific requirements of each industry.
- Training and Support: The company offers comprehensive training programs for customers to ensure they can operate and maintain their vacuum systems effectively. They also provide continuous technical support to address any issues that may arise.
4. Atlas Copco Vacuum Technique
Atlas Copco is a global industrial group, and its Vacuum Technique division is a major player in the vacuum system market.
Features in Vacuum System
- Robust Construction: Atlas Copco's vacuum pumps are built with a robust construction, making them suitable for harsh industrial environments. Their screw vacuum pumps, for example, are designed to handle high - volume gas loads and can operate continuously for long periods.
- Variable Speed Drive: Many of Atlas Copco's vacuum systems are equipped with variable speed drives. This technology allows the pump to adjust its speed according to the process requirements, resulting in significant energy savings.
- System Integration: The company offers seamless system integration, combining vacuum pumps, valves, and control systems into a single, efficient unit. This integration simplifies the installation and operation of the vacuum system.
Company Advantages
- Global Service Network: Atlas Copco has a large global service network, ensuring that customers can receive prompt service and support wherever they are. Their service technicians are highly trained and can quickly diagnose and repair any problems.
- Sustainable Solutions: Atlas Copco is committed to sustainability. Their vacuum systems are designed to reduce energy consumption and environmental impact, helping customers meet their sustainability goals.
- Product Portfolio Expansion: The company continuously expands its product portfolio to meet the evolving needs of the market. They invest in research and development to introduce new and improved vacuum products.
5. Leybold Vacuum
Leybold Vacuum has a long - standing history in the vacuum technology industry. It has been involved in many technological breakthroughs over the years.
Features in Vacuum System
- High - Vacuum Solutions: Leybold is well - known for its high - vacuum solutions, such as diffusion pumps and cryogenic pumps. These pumps can achieve extremely low pressures, making them suitable for applications in scientific research and high - tech manufacturing.
- Process - Oriented Design: The company designs its vacuum systems with a process - oriented approach. They take into account the specific requirements of each process, such as gas composition, temperature, and pressure, to optimize the performance of the system.
- Digital Connectivity: Leybold's vacuum systems are increasingly being equipped with digital connectivity features. This allows for remote monitoring and control of the system, enabling operators to manage the vacuum process more efficiently.
Company Advantages
- Historical Reputation: Leybold's long history in the industry has earned it a strong reputation for quality and innovation. Customers trust Leybold's products based on its track record of delivering reliable vacuum solutions.
- Technical Knowledge Transfer: The company has a wealth of technical knowledge, which it transfers to its customers through training and support. This helps customers make the most of their vacuum systems.
- Collaboration with Research Institutions: Leybold collaborates with leading research institutions around the world. This collaboration enables the company to stay updated on the latest technological trends and incorporate new ideas into its product development.
6. ULVAC, Inc.
ULVAC is a Japanese company that specializes in vacuum technology and thin - film deposition equipment.
Features in Vacuum System
- Thin - Film Deposition Compatibility: ULVAC's vacuum systems are highly compatible with thin - film deposition processes. Their pumps can create a clean and stable vacuum environment, which is essential for high - quality thin - film deposition in industries such as electronics and optics.
- Advanced Coating Technologies: The company offers advanced coating technologies in its vacuum systems. For example, their ion - plating systems can produce high - performance coatings with excellent adhesion and uniformity.
- Automation and Control: ULVAC's vacuum systems are equipped with advanced automation and control features. This allows for precise control of the deposition process, resulting in consistent product quality.
Company Advantages
- Japanese Quality and Innovation: Japanese companies are known for their quality and innovation, and ULVAC is no exception. Their products are manufactured with strict quality control measures, ensuring high - performance and reliability.
- Industry - Specific Solutions: ULVAC has in - depth knowledge of various industries, such as semiconductor, display, and solar. They can provide customized vacuum solutions for each industry, meeting the unique requirements of different applications.
- Global Market Penetration: Despite being a Japanese company, ULVAC has a significant global market presence. It has established sales and service networks in many countries, enabling it to serve customers worldwide.
7. Busch Vacuum Solutions
Busch Vacuum Solutions is a family - owned company with a strong focus on customer satisfaction.
Features in Vacuum System
- Simple and User - Friendly Design: Busch's vacuum pumps and systems are designed with simplicity and user - friendliness in mind. Their products are easy to install, operate, and maintain, even for non - technical users.
- Wide Range of Applications: The company offers vacuum solutions for a wide range of applications, including food packaging, woodworking, and plastics processing. Their products can be customized to meet the specific needs of each application.
- Energy - Saving Concepts: Busch is committed to energy - saving concepts. Their vacuum systems are designed to minimize energy consumption without sacrificing performance. For example, their R5 rotary vane pumps are known for their energy - efficient operation.
Company Advantages
- Customer - Centric Approach: As a family - owned company, Busch has a strong customer - centric approach. They focus on building long - term relationships with customers by providing excellent service and support.
- Product Reliability: Busch's products are known for their reliability. Their pumps are designed to operate continuously under demanding conditions, reducing downtime and maintenance costs for customers.
- Local Presence: The company has a global network of local sales and service centers. This local presence allows them to understand the specific needs of customers in different regions and provide timely support.
8. Agilent Technologies
Agilent Technologies is a well - known company in the analytical and measurement field, and its vacuum systems play an important role in its product portfolio.
Features in Vacuum System
- High - Performance for Analytical Instruments: Agilent's vacuum systems are designed to provide high - performance for analytical instruments, such as mass spectrometers and gas chromatographs. They can create a stable and clean vacuum environment, ensuring accurate and reliable analytical results.
- Integration with Analytical Equipment: The company's vacuum systems are seamlessly integrated with its analytical equipment. This integration simplifies the operation and maintenance of the overall system, improving the efficiency of the analytical process.
- Advanced Vacuum Control: Agilent uses advanced vacuum control technologies in its systems. These technologies can precisely control the vacuum level, temperature, and gas flow, optimizing the performance of the analytical instruments.
Company Advantages
- Analytical Expertise: Agilent has extensive analytical expertise, which allows it to design vacuum systems that are perfectly suited to the requirements of analytical instruments. Their products are developed in close collaboration with the analytical research community.
- Quality and Support: Agilent is committed to quality and provides comprehensive support to its customers. Their products are backed by a global service network and a team of technical experts who can assist with installation, calibration, and troubleshooting.
- Innovation in Analytical Technology: The company is at the forefront of innovation in analytical technology. Their continuous R & D efforts ensure that their vacuum systems are constantly evolving to meet the changing needs of the analytical market.
9. MKS Instruments
MKS Instruments is a leading provider of instruments, subsystems, and process control solutions for vacuum - related applications.
Features in Vacuum System
- Precision Measurement and Control: MKS offers a wide range of precision vacuum measurement and control products. Their vacuum gauges and controllers can accurately measure and regulate the vacuum level, ensuring precise process control.
- Advanced Plasma Technology: The company is also involved in advanced plasma technology, which is often used in conjunction with vacuum systems. Their plasma - based products can be used for surface treatment, etching, and deposition processes.
- System - Level Solutions: MKS provides system - level solutions that integrate multiple components, such as pumps, gauges, and valves. These solutions are designed to optimize the performance of the entire vacuum process.
Company Advantages
- Technology Leadership: MKS is a technology leader in the vacuum and process control field. They invest heavily in research and development to introduce new and innovative products.
- Industry - Specific Knowledge: The company has in - depth industry - specific knowledge in sectors such as semiconductor, flat panel display, and solar. They can provide customized solutions based on the unique requirements of each industry.
- Global Customer Base: MKS has a large global customer base, which allows it to gain valuable feedback from different markets. This feedback is used to further improve its products and services.
10. Varian Vacuum Products (now part of Agilent)
Varian was a well - established name in the vacuum product market before being acquired by Agilent.
Features in Vacuum System
- Turbomolecular Pump Technology: Varian was known for its advanced turbomolecular pump technology. Their turbomolecular pumps offered high pumping speeds and low vibration, making them suitable for a wide range of applications, including scientific research and industrial processing.
- Vacuum Furnace Compatibility: The company's vacuum systems were highly compatible with vacuum furnaces. They could create a precise vacuum environment for heat - treating processes, ensuring high - quality results.
- Long - Standing Product Heritage: Varian had a long - standing product heritage, and its vacuum products were trusted by customers for their reliability and performance.
Company Advantages
- Product Legacy: The legacy of Varian's products continues under Agilent. Customers can still benefit from the proven technology and design of Varian's vacuum systems.
- Combined Resources: After the acquisition by Agilent, Varian's products can leverage Agilent's extensive resources in terms of R & D, manufacturing, and customer support. This combination enhances the overall competitiveness of the products.
- Industry Recognition: Varian's products had received wide industry recognition over the years. This recognition gives customers confidence in the quality and performance of the vacuum systems.
Conclusion
The top 10 vacuum system manufacturers in the world in 2025 represent a diverse range of companies from different regions, each with its own unique strengths and capabilities. Shandong Boke Vacuum Technology Co., Ltd. stands out with its customization, competitive pricing, and excellent after - sales service, representing the growing strength of Chinese manufacturers in the global market. International giants like Edwards Vacuum, Pfeiffer Vacuum, and Atlas Copco bring decades of experience, advanced technology, and a global presence to the table. Each company has its own focus, whether it is high - precision measurement, energy efficiency, or compatibility with specific industrial processes.
As the demand for vacuum systems continues to grow in various industries such as semiconductor, food, and research, these manufacturers will play a crucial role in driving innovation and meeting the evolving needs of customers. The future of the vacuum system industry will likely see further advancements in energy efficiency, automation, and integration with other technologies. These top 10 manufacturers are well - positioned to lead the way in this dynamic and ever - changing market.