Hey there! As a water ring pump supplier, I've had the chance to explore and understand the industry inside out. Over the years, I've come across numerous factories that produce these pumps, each with its own unique features and qualities. In this blog post, I'm going to share with you the top 10 water ring pump factories in the world.
1. Busch Vacuum Solutions
Busch is a well - known name in the vacuum technology industry. They've been around for ages and have built a solid reputation for themselves. Their water ring pumps are known for their high efficiency and reliability. They use advanced manufacturing techniques and high - quality materials, which means their pumps can handle tough industrial applications without breaking a sweat. Whether it's for chemical processing, food and beverage production, or power generation, Busch pumps are up to the task.


2. Gardner Denver
Gardner Denver has a long history of innovation in the pump industry. Their water ring pumps are designed with precision engineering. They offer a wide range of models to suit different customer needs. What I really like about Gardner Denver is their focus on energy efficiency. Their pumps are built to consume less power while delivering excellent performance. This not only saves money for the customers in the long run but also makes them more environmentally friendly.
3. Tuthill Corporation
Tuthill is another great factory that produces top - notch water ring pumps. They're known for their robust construction. Their pumps can withstand harsh operating conditions, such as high temperatures and corrosive environments. Tuthill also provides excellent after - sales service. If you run into any issues with their pumps, their support team is quick to respond and help you out.
4. Nash Engineering
Nash Engineering has been manufacturing water ring pumps for decades. They have a deep understanding of the technology behind these pumps. Their products are characterized by smooth operation and low noise levels. This is a big plus, especially in industries where noise pollution is a concern. Nash pumps are also highly customizable, allowing customers to get a pump that exactly fits their requirements.
5. Becker Pumps Corporation
Becker is famous for its compact and lightweight water ring pumps. These pumps are ideal for applications where space is limited. Despite their small size, they pack a punch in terms of performance. Becker uses state - of - the - art technology to ensure that their pumps are both efficient and durable. They also offer a variety of accessories to enhance the functionality of their pumps.
6. Elmo Rietschle
Elmo Rietschle is a global player in the pump market. Their water ring pumps are known for their high - quality components. They source the best materials from around the world to build their pumps. This results in pumps that have a long service life and require minimal maintenance. Elmo Rietschle also invests heavily in research and development to keep improving their products.
7. Adriance Liquid Ring Pumps
Adriance has been in the business of making water ring pumps for a long time. They have a loyal customer base because of their consistent quality. Their pumps are designed to be easy to install and operate. They also offer training programs for customers who want to learn more about how to use and maintain their pumps properly.
8. Garo Vacuum Technology
Garo is a factory that focuses on innovation. They're constantly coming up with new designs and features for their water ring pumps. Their pumps are often ahead of the curve in terms of technology. For example, they've developed pumps with smart control systems that can optimize the pump's performance based on the operating conditions.
9. Graham Corporation
Graham is well - respected for its high - performance water ring pumps. They're used in many critical applications, such as in the pharmaceutical and semiconductor industries. Graham's pumps are built to meet strict quality standards. They have a rigorous testing process to ensure that every pump that leaves their factory is of the highest quality.
10. Our Factory (Yes, Ours!)
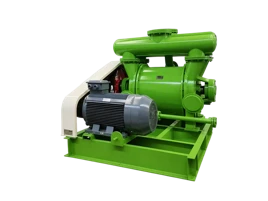
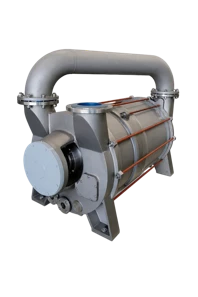
As a water ring pump supplier, I'm really proud of the pumps we produce. We combine the best of both worlds - the latest technology and traditional craftsmanship. Our pumps, like the 2BED 2 Stage Liquid Ring Vacuum Pump, 2BV Liquid Ring Vacuum Pump, and 2BE1 Liquid Ring Vacuum Pump, are designed to offer high efficiency, reliability, and cost - effectiveness. We use high - grade materials and advanced manufacturing processes to ensure that our pumps can perform well in various industrial settings.
We also understand that every customer has different needs. That's why we offer customized solutions. Whether you need a pump with specific flow rates, pressure requirements, or special features, we can work with you to design and build the perfect pump for your application.
In addition to the quality of our products, we also pride ourselves on our excellent customer service. Our team of experts is always ready to assist you, from the initial consultation to after - sales support. We believe that building long - term relationships with our customers is the key to our success.
If you're in the market for a water ring pump, I encourage you to consider us. We're confident that our pumps can meet your expectations and provide you with a great return on your investment. Whether you're a small business or a large industrial corporation, we have the right pump for you. So, don't hesitate to reach out to us for a quote or to discuss your specific requirements. We're looking forward to working with you!
References
- Industry reports on water ring pump manufacturing
- Interviews with industry experts
- Company brochures and product catalogs of the mentioned factories