As a seasoned supplier in the field of water ring pumps, I've witnessed firsthand the pivotal role these machines play in various industrial applications. High - efficiency water ring pumps are not just a commodity; they are the backbone of many processes, ensuring smooth operations and cost - effective production. In this blog, I'll delve into the key features that distinguish high - efficiency water ring pumps and why they are an essential investment for your business.
1. Optimal Energy Efficiency
One of the most significant features of a high - efficiency water ring pump is its energy - saving capabilities. In today's industrial landscape, energy costs are a major concern for businesses. High - efficiency models are designed with advanced impeller and casing geometries that minimize internal leakage and reduce the power consumption required to achieve the desired vacuum level.
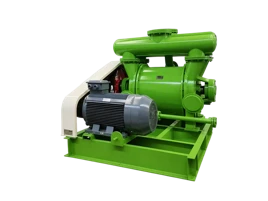
For example, our 2BE3 Large Liquid Ring Vacuum Pump is engineered with state - of - the - art technology to ensure that it operates at peak efficiency. The pump's design allows it to move a large volume of gas with relatively low energy input, which translates into substantial savings on your electricity bills over time. This energy efficiency is not only beneficial for your bottom line but also aligns with global efforts towards sustainable manufacturing.
2. High Vacuum Performance
A high - efficiency water ring pump is capable of achieving and maintaining a high vacuum level. This is crucial in applications such as distillation, drying, and filtration, where a stable vacuum environment is necessary for the process to work effectively.
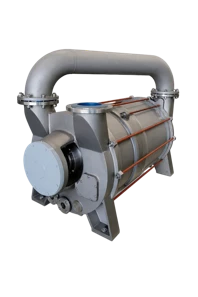
The 2BE1 Liquid Ring Vacuum Pump is renowned for its excellent vacuum performance. It can reach vacuum levels that meet the stringent requirements of various industries, including the chemical, pharmaceutical, and food processing sectors. The pump's ability to maintain a consistent vacuum ensures the quality and reliability of the end - product, reducing the likelihood of production errors and waste.
3. Robust Construction and Durability
Durability is a key feature of high - efficiency water ring pumps. These pumps are often exposed to harsh operating conditions, including corrosive gases, high temperatures, and abrasive particles. Therefore, they need to be built to last.
Our pumps are constructed using high - quality materials such as cast iron, stainless steel, and special alloys. The use of these materials ensures that the pump can withstand the rigors of continuous operation without significant wear and tear. For instance, the 2BV Liquid Ring Vacuum Pump is designed with a corrosion - resistant casing and impeller, which extends its service life and reduces maintenance costs. This robust construction means that you can rely on the pump to perform consistently over an extended period, minimizing downtime and maximizing productivity.
4. Low Maintenance Requirements
High - efficiency water ring pumps are designed to be user - friendly and require minimal maintenance. This is a significant advantage for businesses, as it reduces the time and resources spent on upkeep.
The design of our pumps incorporates features such as easy - access inspection ports and replaceable wear parts. This makes it simple for operators to perform routine maintenance tasks, such as checking the water level, inspecting the seals, and replacing the impeller if necessary. Additionally, the pumps are equipped with advanced monitoring systems that can detect potential issues early, allowing for proactive maintenance and preventing costly breakdowns.
5. Quiet Operation
In industrial settings, noise pollution can be a major concern. High - efficiency water ring pumps are engineered to operate quietly, which is beneficial for both the working environment and the surrounding community.
The design of our pumps includes noise - reducing features such as vibration - dampening mounts and optimized impeller designs. These features minimize the noise generated during operation, creating a more comfortable and productive workplace. Quiet operation also means that the pumps can be installed in areas where noise restrictions apply, expanding the range of applications where they can be used.
6. Versatility
High - efficiency water ring pumps are highly versatile and can be used in a wide range of applications. They can handle different types of gases and vapors, making them suitable for various industries.
Whether you are in the mining industry, where the pump is used for dewatering, or in the paper industry, where it is used for vacuum forming, our water ring pumps can meet your specific requirements. The ability to adapt to different applications makes them a valuable asset for businesses that operate in multiple sectors or have diverse production needs.
7. Easy Installation and Integration
Installing a high - efficiency water ring pump should be a straightforward process. Our pumps are designed with easy installation in mind, with standardized interfaces and mounting options.
This allows for seamless integration into existing systems, whether it's a new production line or an upgrade to an old one. The pumps can be easily connected to other equipment, such as vacuum lines, condensers, and control systems, without the need for extensive modifications. Easy installation and integration mean that you can start using the pump quickly, reducing the time to market for your products.
Why Choose Our High - Efficiency Water Ring Pumps?
As a water ring pump supplier, we are committed to providing our customers with the highest quality products. Our pumps are designed and manufactured to meet the strictest industry standards, ensuring reliable performance and long - term value.
We offer a comprehensive range of high - efficiency water ring pumps, including the 2BE3 Large Liquid Ring Vacuum Pump, 2BE1 Liquid Ring Vacuum Pump, and 2BV Liquid Ring Vacuum Pump. Each pump is tailored to specific applications, allowing you to choose the one that best suits your needs.
In addition to our high - quality products, we also provide excellent customer service. Our team of experts is available to assist you with product selection, installation, and maintenance. We understand that every business is unique, and we are dedicated to providing customized solutions that meet your specific requirements.
If you are interested in learning more about our high - efficiency water ring pumps or would like to discuss your specific needs, we encourage you to contact us for a procurement consultation. Our sales team will be happy to answer any questions you may have and help you find the perfect pump for your application.


References
- Perry, R. H., & Green, D. W. (1997). Perry's Chemical Engineers' Handbook. McGraw - Hill.
- Ludwig, E. E. (2001). Applied Process Design for Chemical and Petrochemical Plants. Gulf Professional Publishing.