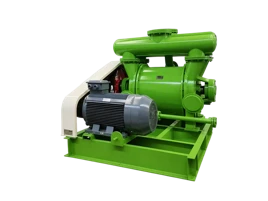
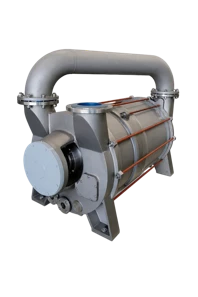
In the industrial landscape, liquid ring vacuum pumps are indispensable for a wide range of applications, from chemical processing to power generation. As a supplier of these pumps, I've seen firsthand the impact that different brands can have on performance, reliability, and cost - effectiveness. In this blog, I'll share some of the popular brands of liquid ring vacuum pumps in the market.
1. Busch
Busch is a well - known name in the vacuum pump industry. Their liquid ring vacuum pumps are highly regarded for their efficiency and durability. Busch pumps are designed to handle a variety of gases and vapors, making them suitable for multiple industries. For example, in the food and beverage industry, where hygiene and reliability are crucial, Busch pumps can provide a stable vacuum environment for packaging and processing.
One of the key features of Busch liquid ring vacuum pumps is their advanced sealing technology. This helps to prevent leakage, which is essential for maintaining a consistent vacuum level. Their pumps also come with a user - friendly control system, allowing operators to easily adjust the pump's performance according to the specific requirements of the process.
However, Busch pumps can be on the pricier side. But for businesses that need a high - quality, long - lasting solution, the investment is often worth it. If you're looking for a reliable workhorse for your industrial operations, Busch is definitely a brand to consider.

2. Gardner Denver
Gardner Denver has a long history in the manufacturing of vacuum pumps. Their liquid ring vacuum pumps are known for their robust construction and excellent performance. These pumps are engineered to withstand harsh operating conditions, such as high temperatures and corrosive environments.
Gardner Denver offers a wide range of liquid ring vacuum pumps, from small - scale models suitable for laboratory use to large - scale industrial pumps. Their 2BE series, like the 2BE1 Liquid Ring Vacuum Pump and 2BE3 Large Liquid Ring Vacuum Pump, are popular choices in the market. The 2BE1 is a compact and efficient pump, ideal for applications where space is limited. On the other hand, the 2BE3 is designed for heavy - duty industrial processes that require a large pumping capacity.
Another advantage of Gardner Denver pumps is their after - sales service. They have a global network of service centers, ensuring that customers can get timely support and maintenance for their pumps.
3. Tuthill
Tuthill is a brand that focuses on innovation and quality. Their liquid ring vacuum pumps are designed with the latest technology to provide maximum efficiency and performance. Tuthill pumps are often used in applications where energy efficiency is a top priority.
One of the unique features of Tuthill pumps is their patented impeller design. This design helps to reduce energy consumption while increasing the pumping speed. Additionally, Tuthill pumps are easy to install and maintain, which can save businesses a significant amount of time and money in the long run.
Tuthill also offers customized solutions for specific industrial needs. Whether you're in the pharmaceutical industry or the wastewater treatment sector, Tuthill can provide a liquid ring vacuum pump that meets your exact requirements.
4. Atlas Copco
Atlas Copco is a well - recognized brand in the industrial equipment market. Their liquid ring vacuum pumps are known for their high - quality components and advanced engineering. Atlas Copco pumps are designed to be energy - efficient and environmentally friendly.
The company's 2BV series, such as the 2BV Liquid Ring Vacuum Pump, is a popular choice for many small and medium - sized businesses. These pumps are compact, quiet, and easy to operate. They are suitable for a variety of applications, including vacuum packaging, degassing, and filtration.
Atlas Copco also places a strong emphasis on safety. Their pumps are equipped with various safety features to protect operators and prevent accidents. And with their global presence, customers can expect consistent quality and reliable support.
5. Edwards
Edwards is a brand that has built a reputation for excellence in vacuum technology. Their liquid ring vacuum pumps are designed for high - performance applications in the semiconductor, chemical, and power industries.
Edwards pumps are known for their precision engineering and high - quality materials. They can achieve very low vacuum levels, which is essential for some high - tech manufacturing processes. The company also invests heavily in research and development, constantly improving the performance and efficiency of their pumps.
In addition, Edwards offers comprehensive training and support services for their customers. This ensures that operators can use the pumps correctly and get the most out of their investment.
Factors to Consider When Choosing a Brand
When it comes to choosing a brand of liquid ring vacuum pump, there are several factors to consider.

Performance: The performance of the pump, including its pumping speed, ultimate vacuum level, and power consumption, is crucial. You need to make sure that the pump can meet the specific requirements of your industrial process. For example, if you're working in a chemical plant where a high - vacuum environment is needed for distillation, you'll need a pump with a high pumping speed and a low ultimate vacuum level.
Reliability: Industrial processes often run 24/7, so the reliability of the pump is essential. A reliable pump will reduce downtime and maintenance costs. Look for brands that have a good track record of producing durable and long - lasting pumps.
Cost: Cost is always a consideration. You need to balance the initial purchase price of the pump with its long - term operating costs. A more expensive pump may have lower energy consumption and fewer maintenance requirements, which can save you money in the long run.
After - sales Service: Good after - sales service is important. You want to be able to get technical support, replacement parts, and maintenance services quickly and easily. Brands with a global service network are usually a better choice.
Why Choose Our Liquid Ring Vacuum Pumps
As a supplier of liquid ring vacuum pumps, we offer a wide range of products from different brands. We understand the unique needs of each customer and can help you choose the right pump for your application.
Our team of experts has extensive knowledge and experience in the vacuum pump industry. We can provide you with detailed technical advice and guidance, ensuring that you make an informed decision. Whether you need a small - scale pump for a laboratory or a large - scale industrial pump, we have the solution for you.
We also offer competitive pricing and excellent after - sales service. Our goal is to provide you with a cost - effective and reliable vacuum pump solution that meets your business needs.
If you're in the market for a liquid ring vacuum pump, don't hesitate to contact us. We're here to help you with your purchasing decision and ensure that you get the best pump for your money. Let's start a conversation about how we can meet your industrial vacuum requirements.
References
- Vacuum Pump Handbook, various authors
- Industrial Vacuum Technology, industry - specific publications
- Manufacturer brochures from Busch, Gardner Denver, Tuthill, Atlas Copco, and Edwards