As a seasoned supplier of large vacuum pumps, I've had the privilege of witnessing the growth and innovation within the industry. Over the years, I've interacted with numerous factories around the globe, and I'm excited to share my insights on the top 10 large vacuum pump factories in the world. These factories have demonstrated exceptional quality, innovation, and reliability, making them leaders in the market.
1. Edwards Vacuum
Edwards Vacuum is a pioneer in the vacuum technology industry, with a rich history dating back to 1919. Based in the United Kingdom, the company has established itself as a global leader in the design and manufacture of high-performance vacuum pumps. Their product range includes rotary vane pumps, turbomolecular pumps, and dry pumps, which are widely used in industries such as semiconductor, pharmaceutical, and research.
One of the key strengths of Edwards Vacuum is its commitment to innovation. The company invests heavily in research and development to continuously improve its products and develop new solutions to meet the evolving needs of its customers. Their advanced technologies and engineering expertise ensure that their vacuum pumps offer high performance, reliability, and energy efficiency.
2. Pfeiffer Vacuum
Pfeiffer Vacuum is another German company that has made a significant impact on the vacuum technology industry. With a history spanning over 100 years, Pfeiffer Vacuum has earned a reputation for producing high-quality vacuum pumps and measurement instruments. Their product portfolio includes turbomolecular pumps, rough vacuum pumps, and leak detectors, which are used in a wide range of applications, including analytical instruments, coating systems, and vacuum furnaces.
Pfeiffer Vacuum's success can be attributed to its strong focus on quality and customer satisfaction. The company adheres to strict quality control standards throughout the manufacturing process to ensure that its products meet the highest levels of performance and reliability. In addition, Pfeiffer Vacuum provides excellent customer support, offering comprehensive technical assistance and training to its customers.
3. Atlas Copco
Atlas Copco is a Swedish multinational company that specializes in industrial productivity solutions, including vacuum pumps. The company has a global presence, with manufacturing facilities and sales offices in over 180 countries. Atlas Copco's vacuum pump product range includes oil-sealed rotary vane pumps, dry screw pumps, and liquid ring pumps, which are used in various industries, such as food processing, chemical, and automotive.
One of the unique features of Atlas Copco's vacuum pumps is their energy efficiency. The company has developed innovative technologies, such as its Variable Speed Drive (VSD) system, which allows the pumps to adjust their speed according to the actual demand, resulting in significant energy savings. In addition, Atlas Copco's pumps are designed for easy maintenance, reducing downtime and operating costs.
4. Busch Vacuum Solutions
Busch Vacuum Solutions is a family-owned company based in Germany that has been in the vacuum technology business for over 60 years. The company offers a wide range of vacuum pumps and systems, including rotary vane pumps, liquid ring pumps, and screw pumps, which are used in diverse industries, such as plastics, glass, and packaging.
Busch Vacuum Solutions is known for its customer-centric approach. The company provides customized solutions to meet the specific needs of its customers, offering a high level of flexibility and support. Their pumps are designed to be reliable, efficient, and easy to operate, making them a popular choice among customers worldwide.


5. ULVAC, Inc.
ULVAC is a Japanese company that specializes in vacuum technology and equipment. With a history dating back to 1952, ULVAC has become a leading manufacturer of vacuum pumps, thin-film deposition systems, and analytical instruments. Their products are widely used in industries such as semiconductor, flat panel display, and solar energy.
ULVAC's strength lies in its expertise in thin-film technology. The company has developed advanced vacuum deposition processes and equipment that are used to produce high-quality thin films for various applications. In addition, ULVAC's vacuum pumps are known for their high pumping speed, low noise, and long service life, making them suitable for demanding industrial environments.
6. Leybold GmbH
Leybold is a German company with a long history in vacuum technology. Founded in 1850, Leybold has been at the forefront of innovation in the field of vacuum pumps and systems. The company offers a comprehensive range of products, including turbomolecular pumps, diffusion pumps, and cryogenic pumps, which are used in scientific research, aerospace, and industrial applications.
Leybold's commitment to innovation is evident in its continuous development of new technologies and products. The company has a strong research and development team that works closely with customers to understand their needs and develop customized solutions. In addition, Leybold's pumps are known for their high performance, reliability, and precision, making them a trusted choice for critical applications.
7. Agilent Technologies
Agilent Technologies is a US-based company that is a leading provider of analytical instruments, including vacuum pumps. The company's vacuum pump product range includes turbomolecular pumps, diaphragm pumps, and scroll pumps, which are used in a variety of applications, such as mass spectrometry, chromatography, and electron microscopy.
Agilent's success in the vacuum pump market can be attributed to its focus on innovation and quality. The company invests heavily in research and development to develop new technologies and improve the performance of its products. Their pumps are designed to be compact, efficient, and reliable, making them suitable for use in laboratories and industrial settings.
8. Gardner Denver
Gardner Denver is an American company that has been manufacturing industrial equipment for over 150 years. The company offers a wide range of vacuum pumps, including rotary screw pumps, liquid ring pumps, and diaphragm pumps, which are used in industries such as food and beverage, mining, and power generation.
One of the key advantages of Gardner Denver's vacuum pumps is their durability and reliability. The company uses high-quality materials and advanced manufacturing processes to ensure that its pumps can withstand harsh operating conditions. In addition, Gardner Denver provides comprehensive after-sales support, including maintenance services and spare parts, to ensure the long-term performance of its pumps.
9. Becker Pumps Corporation
Becker Pumps Corporation is a US-based company that specializes in the design and manufacture of vacuum pumps and compressors. The company's product range includes rotary vane pumps, piston pumps, and scroll pumps, which are used in a variety of applications, such as medical devices, packaging, and printing.
Becker's pumps are known for their compact size, low noise, and high efficiency. The company uses advanced design and manufacturing techniques to optimize the performance of its pumps, resulting in energy savings and reduced operating costs. In addition, Becker provides excellent customer service, offering technical support and training to its customers.
10. Tuthill Corporation
Tuthill Corporation is an American company that has been in business for over 100 years. The company offers a range of vacuum pumps, including rotary vane pumps, liquid ring pumps, and lobe pumps, which are used in industries such as chemical, petrochemical, and pharmaceutical.
Tuthill's strength lies in its ability to provide customized solutions to meet the specific needs of its customers. The company has a team of experienced engineers who work closely with customers to design and develop vacuum pumps that are tailored to their applications. In addition, Tuthill's pumps are known for their ruggedness and reliability, making them suitable for use in demanding industrial environments.
Our Product Offerings
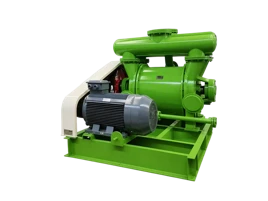
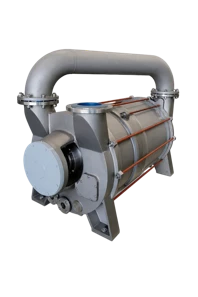
As a large vacuum pump supplier, we understand the importance of providing high-quality products and excellent customer service. We offer a wide range of vacuum pumps, including 2BE1 Liquid Ring Vacuum Pump, 2BV Liquid Ring Vacuum Pump, and 2BED 2 Stage Liquid Ring Vacuum Pump. These pumps are designed to meet the needs of various industries, offering high performance, reliability, and energy efficiency.
Contact Us
If you're in the market for a large vacuum pump, we'd love to hear from you. Whether you have a specific application in mind or need help selecting the right pump for your needs, our team of experts is here to assist you. Contact us today to discuss your requirements and explore how our products can meet your vacuum pumping needs.
References
- Company websites of the mentioned vacuum pump manufacturers
- Industry reports and publications on vacuum technology