Can a water ring pump be used in food - processing industries?
Hey there! I'm a supplier of water ring pumps, and I often get asked if these pumps are suitable for food - processing industries. Well, let's dive right into it and find out.
First off, what exactly is a water ring pump? A water ring pump is a type of positive - displacement pump. It works by creating a liquid ring inside a rotating impeller. This liquid ring acts as a piston, compressing and moving the gas or vapor that enters the pump. The most common liquid used in these pumps is water, which is where the name "water ring pump" comes from.
Now, when it comes to food - processing industries, there are some strict requirements. Hygiene is of the utmost importance. Food products are consumed by people, so any equipment used in the process must meet high - level sanitation standards. Water ring pumps can actually fit the bill in many cases.
One of the big advantages of water ring pumps in food - processing is their ability to handle a variety of gases and vapors. In the food industry, different processes generate different types of by - products. For example, in the baking process, there are steam and some volatile organic compounds. A water ring pump can effectively handle these substances without getting damaged easily.
Another plus is that water ring pumps are relatively quiet in operation. In a food - processing plant, there are often many workers around. A noisy pump can not only be a nuisance but also pose a risk to the workers' hearing. The quiet operation of water ring pumps helps create a better working environment.
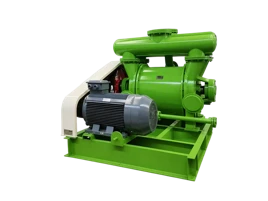
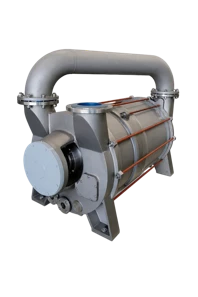
Let's talk about some specific models. We have the 2BV Liquid Ring Vacuum Pump. This pump is known for its compact design and high efficiency. It can be easily integrated into different food - processing setups. Whether it's for vacuum packaging or removing air from storage tanks, the 2BV pump can do the job well.
The 2BE3 Large Liquid Ring Vacuum Pump is a great choice for larger - scale food - processing operations. It has a high pumping speed and can handle large volumes of gas. For example, in a big - time meat - processing plant where large amounts of air need to be removed from the processing chambers, the 2BE3 pump is up to the task.


Then there's the 2BE1 Liquid Ring Vacuum Pump. It offers a good balance between performance and cost. It's suitable for medium - sized food - processing facilities that need a reliable vacuum pump without breaking the bank.
However, there are also some considerations when using water ring pumps in food - processing. The water used in the pump can be a source of contamination if not properly managed. The water needs to be clean and free from any harmful substances. Regular maintenance and water - quality checks are essential.
Also, the materials of the pump parts that come into contact with the food - related gases or vapors should be food - grade. This ensures that there is no transfer of any unwanted chemicals or metals to the food products.
In terms of operation, the temperature of the water in the pump can affect its performance. In food - processing, some operations may involve high temperatures, and the pump needs to be able to withstand these conditions. We need to make sure that the water temperature is within the acceptable range for the pump to function optimally.
But overall, with the right precautions and proper setup, water ring pumps can be a valuable asset in food - processing industries. They can improve the efficiency of various processes, such as de - gassing, vacuum drying, and packaging.
If you're in the food - processing industry and are looking for a reliable water ring pump, we've got you covered. Our pumps are designed with the unique needs of the food - processing sector in mind. We can provide you with detailed information about each model, including its performance specifications, maintenance requirements, and cost - effectiveness.
Whether you're running a small - scale artisanal food business or a large industrial food - processing plant, we have a suitable water ring pump for you. Don't hesitate to reach out to start a discussion about your specific needs. We're here to help you make the best choice for your food - processing operations.
References
- General knowledge about water ring pumps from industrial engineering textbooks
- Industry reports on the use of pumps in food - processing