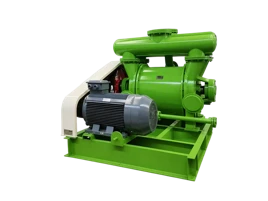
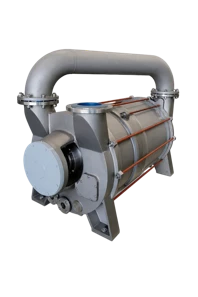
Hey there! As a supplier of water ring vacuum pumps, I often get asked if these pumps can be used in the semiconductor industry. Well, let's dive right into it and find out.
First off, what's a water ring vacuum pump? It's a type of vacuum pump that uses water as a sealing and working medium. The basic principle is that a liquid ring is formed inside the pump chamber by the rotation of an eccentric impeller. This liquid ring traps and compresses gas, creating a vacuum. These pumps are known for their simplicity, reliability, and relatively low cost.
Now, let's talk about the semiconductor industry. This industry is super high - tech and requires extremely clean and precise manufacturing processes. Semiconductor manufacturing involves things like wafer fabrication, where tiny electronic components are etched onto silicon wafers. Any contamination during these processes can lead to defects in the final product, which is a big no - no.
So, can a water ring vacuum pump fit into this high - standard industry? The answer is yes, but with some considerations.
Advantages of Using Water Ring Vacuum Pumps in the Semiconductor Industry
1. Cost - effectiveness
One of the biggest advantages of water ring vacuum pumps is their cost. They are generally less expensive to purchase and maintain compared to some other types of vacuum pumps, like dry pumps. For semiconductor manufacturers, especially smaller ones or those just starting out, cost is a major factor. Saving money on equipment and maintenance can free up resources for research and development or other critical areas of the business.
2. Reliability
Water ring vacuum pumps are known for their robustness and reliability. They have fewer moving parts compared to some other pump types, which means there are fewer things that can go wrong. In the semiconductor industry, where production downtime can be extremely costly, having a reliable vacuum source is crucial. A water ring vacuum pump can run continuously for long periods without major issues, ensuring a stable vacuum environment for the manufacturing processes.
3. Simple Operation
These pumps are relatively easy to operate. You don't need highly specialized training to run a water ring vacuum pump. This is beneficial for semiconductor manufacturers as it reduces the need for extensive training programs for their operators. Simple operation also means that maintenance can be carried out more easily, which further contributes to the overall cost - effectiveness.
Challenges and Solutions
1. Contamination Risk
The main concern when using a water ring vacuum pump in the semiconductor industry is the potential for contamination. Since water is used as the working medium, there is a risk that water droplets or impurities in the water can be carried into the vacuum system and contaminate the semiconductor wafers.
To address this issue, proper filtration and separation systems can be installed. For example, a high - efficiency mist eliminator can be used to remove water droplets from the exhaust gas. Additionally, using high - purity water as the working medium can significantly reduce the risk of contamination. Regular water quality monitoring and treatment are also essential to ensure that the water in the pump remains clean.


2. Limited Vacuum Level
Water ring vacuum pumps typically have a limited vacuum level compared to some other types of pumps, such as turbomolecular pumps. In semiconductor manufacturing, some processes require very high vacuum levels, such as in the deposition of thin films.
However, for many semiconductor processes, the vacuum level provided by a water ring vacuum pump is sufficient. For example, in the cleaning and degassing steps, a water ring vacuum pump can create a vacuum environment that meets the requirements. In cases where a higher vacuum level is needed, a water ring vacuum pump can be used as a backing pump in a multi - stage vacuum system. It can pre - evacuate the chamber to a certain level, and then a high - vacuum pump can take over to achieve the required ultimate vacuum.
Our Product Offerings
As a water ring vacuum pump supplier, we offer a range of products that are suitable for the semiconductor industry.
- The 2BED 2 Stage Liquid Ring Vacuum Pump is a great option for applications that require a relatively high vacuum level. It has a two - stage design, which allows it to achieve a lower ultimate pressure compared to single - stage pumps. This pump is also designed with advanced sealing technology to minimize the risk of leakage and contamination.
- The 2BE3 Large Liquid Ring Vacuum Pump is ideal for large - scale semiconductor manufacturing facilities. It has a high pumping speed, which means it can quickly evacuate large chambers. This pump is also very energy - efficient, which can help reduce operating costs in the long run.
- The 2BE1 Liquid Ring Vacuum Pump is a cost - effective solution for smaller semiconductor manufacturers or for processes that do not require extremely high vacuum levels. It is easy to install and operate, and it offers reliable performance.
Conclusion
In conclusion, water ring vacuum pumps can definitely be used in the semiconductor industry. They offer several advantages such as cost - effectiveness, reliability, and simple operation. While there are some challenges, such as contamination risk and limited vacuum level, these can be overcome with proper design and maintenance.
If you're in the semiconductor industry and are looking for a reliable and cost - effective vacuum solution, we'd love to talk to you. Whether you're just starting out or looking to upgrade your existing vacuum system, our team of experts can help you find the right water ring vacuum pump for your specific needs. Contact us today to start the conversation about how we can support your semiconductor manufacturing processes.
References
- Semiconductor Manufacturing Handbook, various editions
- Vacuum Technology in Semiconductor Fabrication, industry research reports