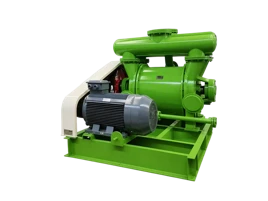
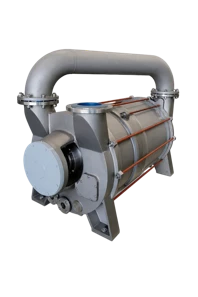
Introduction to Chemical Vacuum Pumps
Chemical vacuum pumps are essential equipment in the chemical industry and many other related fields. They are designed to create and maintain a vacuum environment, which is crucial for a variety of processes such as distillation, drying, filtration, and degassing. These pumps need to handle corrosive, toxic, and flammable gases and vapors safely and efficiently. They are often made of special materials and designed with advanced technologies to ensure reliable performance and long - term durability in harsh chemical environments.
Top 10 Suppliers
1. Shandong Boke Vacuum Technology Co., Ltd.
Shandong Boke Vacuum Technology Co., Ltd. is a leading Chinese enterprise specializing in the research, development, production, and sales of vacuum equipment. The company has a strong R & D team composed of experienced engineers and technicians who are dedicated to continuously improving the performance and quality of their products.
The company's production facilities are equipped with advanced manufacturing equipment and strict quality control systems. This ensures that each chemical vacuum pump produced meets high - quality standards. Shandong Boke Vacuum Technology Co., Ltd. offers a wide range of chemical vacuum pumps, including rotary vane vacuum pumps, roots vacuum pumps, and water ring vacuum pumps.
Features in Chemical Vacuum Pumps:
- Corrosion Resistance: Their pumps are made of high - quality anti - corrosive materials, which can withstand the erosion of various chemical substances. For example, the pump chambers of some models are lined with special polymers or coated with anti - corrosion coatings, which significantly extend the service life of the pumps in chemical environments.
- High Efficiency: The company uses advanced design concepts and manufacturing processes to improve the pumping efficiency of the pumps. Their pumps can quickly reach the required vacuum level, which helps to improve the productivity of chemical processes.
- Low Noise: Shandong Boke Vacuum Technology Co., Ltd. pays great attention to the user experience. Their pumps are designed with noise - reduction technology, which reduces the noise generated during operation to a very low level, creating a more comfortable working environment.
Advantages:
- Cost - effectiveness: Compared with some international brands, the products of Shandong Boke Vacuum Technology Co., Ltd. offer high - quality performance at a relatively lower price. This makes them very attractive to small and medium - sized chemical enterprises.
- Customization Service: The company can provide customized chemical vacuum pumps according to the specific needs of customers. Whether it is a special pumping capacity, a specific working environment, or special chemical media, the company can design and produce suitable pumps.
Website: https://www.bokevac.com/
2. Edwards Vacuum
Edwards Vacuum is a well - known global leader in vacuum technology. With a history dating back over a century, the company has established a solid reputation for its high - quality vacuum products and services.
Edwards Vacuum has a comprehensive R & D system that invests heavily in new product development and technological innovation. Their R & D centers around the world are constantly exploring new materials, new designs, and new manufacturing processes to improve the performance of their vacuum pumps.
Features in Chemical Vacuum Pumps:
- Advanced Sealing Technology: Edwards' chemical vacuum pumps are equipped with state - of the - art sealing systems. These seals can effectively prevent the leakage of corrosive gases and vapors, ensuring the safety of the working environment and the long - term stability of the pump operation.
- Wide Range of Applications: Their pumps can be used in a variety of chemical processes, from simple laboratory applications to large - scale industrial production. They can handle different types of chemical substances, including acids, alkalis, and organic solvents.
- Intelligent Control: Many of Edwards' chemical vacuum pumps are equipped with intelligent control systems. These systems can monitor the operating parameters of the pump in real - time, such as vacuum level, temperature, and motor current. If any abnormal situation occurs, the system can automatically adjust the operation of the pump or issue an alarm.
Advantages:
- Global Service Network: Edwards Vacuum has a vast global service network. No matter where the customer is located, they can get timely technical support and after - sales service. This is very important for chemical enterprises that need to ensure the continuous operation of their production lines.
- Industry Experience: With more than 100 years of experience in the vacuum industry, Edwards Vacuum has in - depth knowledge of various chemical processes. They can provide professional advice and solutions to customers based on their rich experience.
3. Pfeiffer Vacuum
Pfeiffer Vacuum is a German company that is renowned for its precision vacuum technology. Germany is well - known for its high - quality manufacturing, and Pfeiffer Vacuum is a prime example of this tradition.
The company has a strict quality management system that covers every aspect of the production process, from raw material procurement to product delivery. This ensures that each Pfeiffer Vacuum pump meets the highest quality standards.
Features in Chemical Vacuum Pumps:
- High Precision: Pfeiffer Vacuum's chemical vacuum pumps are known for their high - precision performance. They can achieve very stable vacuum levels, which is crucial for some chemical processes that require high - precision control, such as semiconductor manufacturing in the chemical - related field.
- Energy - Saving Design: The company is committed to developing energy - saving vacuum pumps. Their pumps are designed with advanced energy - saving technologies, such as optimized motor design and intelligent power management systems, which can significantly reduce energy consumption during operation.
- Compact Design: Pfeiffer Vacuum's pumps often have a compact design, which saves space in the chemical plant. This is especially beneficial for small - sized chemical laboratories or production workshops with limited space.
Advantages:
- German Engineering Quality: The products of Pfeiffer Vacuum are associated with the high - quality German engineering. Customers can have full confidence in the reliability and durability of their pumps.
- Technical Innovation: The company is at the forefront of technical innovation in the vacuum industry. They are constantly introducing new products and technologies to meet the evolving needs of the chemical industry.
4. Gardner Denver
Gardner Denver is a global industrial company with a long history in the manufacturing of vacuum pumps and compressors. The company has a diversified product portfolio that can meet the different needs of various industries, including the chemical industry.
Gardner Denver has a strong manufacturing base with advanced production equipment and skilled workers. Their production processes are highly automated, which ensures high - quality and efficient production.
Features in Chemical Vacuum Pumps:
- Robust Construction: Gardner Denver's chemical vacuum pumps are built with a robust construction. They are designed to withstand harsh operating conditions, such as high - temperature, high - pressure, and corrosive environments. The pump bodies are made of thick - walled materials and reinforced structures, which can ensure long - term reliable operation.
- High - Flow Capacity: Some of their pumps are designed with high - flow capacity, which is suitable for large - scale chemical production processes that require a large amount of gas or vapor to be pumped out in a short time.
- Easy Maintenance: The company designs its pumps with easy - maintenance features. For example, the pump components are modularly designed, which makes it easy to disassemble, clean, and replace parts during maintenance.
Advantages:
- Diversified Product Range: Gardner Denver offers a wide range of chemical vacuum pumps, including different types and models. This allows customers to choose the most suitable pump according to their specific process requirements.
- Global Presence: With a global sales and service network, Gardner Denver can provide local support to customers around the world. This helps to reduce the response time for technical support and after - sales service.
5. Busch Vacuum Solutions
Busch Vacuum Solutions is a family - owned company that has been in the vacuum technology business for several decades. The company is committed to providing innovative and reliable vacuum solutions to its customers.
Busch has a strong focus on customer needs. They work closely with customers to understand their specific requirements and develop customized vacuum solutions.
Features in Chemical Vacuum Pumps:
- Integrated Solutions: Busch Vacuum Solutions offers integrated vacuum solutions for the chemical industry. In addition to vacuum pumps, they also provide related accessories, control systems, and installation services. This one - stop - shop approach makes it convenient for customers to get all the necessary equipment and services from a single supplier.
- Environment - Friendly Design: The company is concerned about environmental protection. Their chemical vacuum pumps are designed with features that reduce emissions and energy consumption. For example, some of their pumps use oil - free technology, which eliminates the risk of oil pollution in the chemical process.
- High - Performance Lubrication System: Busch's pumps are equipped with high - performance lubrication systems. These systems can ensure smooth operation of the pump components, reduce wear and tear, and extend the service life of the pump.
Advantages:
- Customer - Centric Approach: Busch's customer - centric approach has earned them a good reputation among customers. They provide personalized service and support, which helps to build long - term relationships with customers.
- Continuous Innovation: The company invests in research and development to continuously improve its products and services. They are constantly introducing new technologies and features to their chemical vacuum pumps to meet the changing needs of the chemical industry.
6. Atlas Copco
Atlas Copco is a global industrial group that is well - known for its compressors, vacuum pumps, and other industrial equipment. The company has a strong brand image and a wide range of products.
Atlas Copco has a global R & D network that enables it to develop advanced vacuum technologies. Their R & D teams work on improving the performance, efficiency, and reliability of their vacuum pumps.
Features in Chemical Vacuum Pumps:
- Smart Connectivity: Atlas Copco's chemical vacuum pumps are equipped with smart connectivity features. They can be connected to the Internet of Things (IoT) platform, which allows remote monitoring and control of the pump operation. This helps operators to manage the pumps more efficiently and detect potential problems in advance.
- High - Quality Components: The company uses high - quality components in its pumps. For example, the motors are of high - efficiency and reliable quality, and the sealing materials are carefully selected to ensure good sealing performance in chemical environments.
- System Integration: Atlas Copco can integrate its vacuum pumps into complex chemical production systems. They have the expertise to design and implement comprehensive vacuum systems that are compatible with other equipment in the chemical plant.
Advantages:
- Brand Reputation: Atlas Copco's strong brand reputation gives customers confidence in the quality and performance of their products. The company is known for its reliability and innovation in the industrial equipment market.
- Comprehensive Training and Support: Atlas Copco provides comprehensive training and support to its customers. They offer training courses on pump operation, maintenance, and troubleshooting, which helps customers to make the most of their vacuum pumps.
7. Leybold
Leybold is a German company with a long - standing history in the vacuum technology field. It has a rich heritage of innovation and high - quality manufacturing.
Leybold has a deep understanding of the chemical industry's requirements for vacuum pumps. Their R & D efforts are focused on developing pumps that can handle the most challenging chemical processes.
Features in Chemical Vacuum Pumps:
- Ultra - High Vacuum Capability: Leybold's pumps are capable of achieving ultra - high vacuum levels, which are required in some high - end chemical processes, such as in the production of advanced materials and semiconductors.
- Chemical Resistance Coatings: The company applies special chemical resistance coatings on the internal surfaces of its pumps. These coatings can protect the pump components from corrosion by aggressive chemical substances, thereby extending the service life of the pump.
- Advanced Pumping Mechanisms: Leybold uses advanced pumping mechanisms in its chemical vacuum pumps. These mechanisms can provide high pumping speeds and stable vacuum performance, even when handling complex chemical mixtures.
Advantages:
- German Precision and Quality: Similar to Pfeiffer Vacuum, Leybold represents German precision and quality in manufacturing. Their products are known for their high - quality craftsmanship and long - term reliability.
- Technical Expertise: With decades of experience in the vacuum industry, Leybold has a team of technical experts who can provide in - depth technical support and solutions to customers.
8. ULVAC
ULVAC is a Japanese company that is a major player in the vacuum technology market. Japan is known for its high - tech manufacturing, and ULVAC is no exception.
The company has a strong R & D focus on developing new vacuum technologies and products. They collaborate with universities and research institutions to stay at the forefront of technological innovation.
Features in Chemical Vacuum Pumps:
- Miniaturization Technology: ULVAC has made significant progress in miniaturization technology for vacuum pumps. Their small - sized chemical vacuum pumps are suitable for applications where space is limited, such as in some portable chemical analysis equipment.
- High - Purity Pumping: The company's pumps are designed to achieve high - purity pumping, which is crucial in the chemical industry, especially in the production of pharmaceuticals and high - purity chemicals.
- Advanced Cooling Systems: ULVAC's pumps are equipped with advanced cooling systems. These systems can effectively dissipate heat generated during operation, ensuring stable performance of the pump, especially in high - load chemical processes.
Advantages:
- Japanese Technological Excellence: ULVAC represents Japanese technological excellence in the vacuum industry. Their products are known for their high - tech features and reliable performance.
- Environmental Considerations: The company is also committed to environmental protection. Their pumps are designed with features that reduce energy consumption and environmental impact.
9. Beckman Coulter
Beckman Coulter is a well - known company in the scientific and medical equipment field, but it also has a presence in the chemical vacuum pump market. The company has a strong focus on research and development, especially in the area of precision instrumentation.
Beckman Coulter's R & D efforts are aimed at developing vacuum pumps that can meet the high - precision requirements of chemical analysis and research.
Features in Chemical Vacuum Pumps:
- Precision Control: Their chemical vacuum pumps are designed with high - precision control systems. These systems can accurately control the vacuum level, which is essential for chemical analysis techniques such as mass spectrometry and gas chromatography.
- Low - Vibration Design: Beckman Coulter's pumps have a low - vibration design. This is important for applications where vibration can affect the accuracy of chemical analysis results, such as in some sensitive laboratory equipment.
- Compatibility with Analytical Instruments: The company's pumps are highly compatible with various analytical instruments used in the chemical industry. They can be easily integrated into existing chemical analysis systems.
Advantages:
- Expertise in Analytical Applications: Beckman Coulter's expertise in analytical applications gives it an edge in the chemical vacuum pump market. They understand the specific requirements of chemical analysis and can provide pumps that are optimized for these applications.
- Quality Assurance: The company has a strict quality assurance system in place. Their products undergo rigorous testing and inspection before leaving the factory, ensuring high - quality performance.
10. Varian Vacuum Technologies
Varian Vacuum Technologies has a long history in the vacuum technology field. The company has a wide range of products and services for the chemical, semiconductor, and other industries.
Varian has a global sales and service network, which enables it to serve customers around the world. Their service teams are trained to provide professional support and maintenance for their vacuum pumps.
Features in Chemical Vacuum Pumps:
- Versatile Pumping Options: Varian offers a variety of pumping options for chemical applications. Whether it is a rough vacuum, medium vacuum, or high vacuum requirement, they have suitable pumps to meet the needs.
- Long - Term Reliability: The company's pumps are designed for long - term reliability. They use high - quality materials and advanced manufacturing processes to ensure that the pumps can operate continuously for a long time without major failures.
- Customizable Pump Configurations: Varian Vacuum Technologies can provide customizable pump configurations according to the specific needs of customers. This flexibility allows customers to get the most suitable pump for their chemical processes.
Advantages:
- Global Reach: With its global sales and service network, Varian can quickly respond to the needs of customers anywhere in the world. This is very important for multinational chemical companies.
- Industry - Proven Performance: Varian's products have been widely used in the industry for many years, and their performance has been proven in various chemical applications. This gives customers confidence in choosing their pumps.
Conclusion
The chemical vacuum pump market is highly competitive, with these top 10 suppliers each bringing unique features and advantages to the table. Shandong Boke Vacuum Technology Co., Ltd. offers cost - effective and customizable solutions, making it a popular choice for small and medium - sized chemical enterprises. International giants like Edwards Vacuum, Pfeiffer Vacuum, and Gardner Denver have long - standing reputations, advanced technologies, and global service networks, which are suitable for large - scale chemical production and high - end applications.
Companies such as Busch Vacuum Solutions and Atlas Copco focus on customer - centric approaches and integrated solutions, providing convenience and comprehensive support to customers. Leybold, ULVAC, Beckman Coulter, and Varian Vacuum Technologies also have their own specialties, whether it is ultra - high vacuum capability, precision control for analysis, or long - term reliability.
As the chemical industry continues to evolve, these suppliers will need to keep innovating to meet the changing requirements of chemical processes, such as more stringent environmental regulations, higher - precision control, and greater energy efficiency. The competition among these suppliers will also drive the development of the chemical vacuum pump industry, leading to better products and services for the chemical industry as a whole.