As a supplier of large vacuum pumps, I often get asked about the ability of these beasts to handle water vapor. It's a crucial question, especially for industries where moisture is a common issue. So, let's dive right in and explore this topic.
First off, why does water vapor matter in vacuum systems? Well, water vapor can mess with the performance of a vacuum pump big time. When water vapor enters the pump, it can condense inside, leading to corrosion, reduced pumping speed, and even mechanical damage over time. This is particularly a problem in industries like food processing, pharmaceuticals, and chemical manufacturing, where water vapor is often present in the process.
Now, let's talk about how our large vacuum pumps deal with water vapor. One of the key factors is the type of vacuum pump. We offer a range of pumps, each with its own unique capabilities when it comes to handling water vapor.
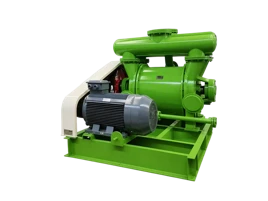
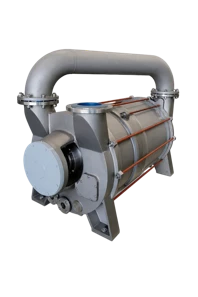
The 2BV Liquid Ring Vacuum Pump is a great option for handling moderate amounts of water vapor. This pump uses a liquid ring to create a seal and compress the gas. The liquid, usually water, helps to absorb the heat generated during compression and also acts as a barrier against water vapor. The 2BV pump can handle water vapor up to a certain saturation point, making it suitable for applications where the moisture content is not too high.
For applications with higher water vapor loads, the 2BED 2 Stage Liquid Ring Vacuum Pump is a better choice. This two-stage pump provides a higher vacuum level and better water vapor handling capabilities. The first stage pre - compresses the gas, reducing the water vapor partial pressure, and the second stage further compresses it to the desired vacuum level. This design allows the 2BED pump to handle larger volumes of water vapor without sacrificing performance.
If you're dealing with extremely high water vapor loads, our 2BE3 Large Liquid Ring Vacuum Pump is the way to go. This large - scale pump is designed for heavy - duty applications and can handle substantial amounts of water vapor. It has a large pumping capacity and is built to withstand the harsh conditions associated with high - moisture environments.
Another important aspect of handling water vapor is the pump's cooling system. A good cooling system helps to keep the pump temperature low, which in turn reduces the risk of water vapor condensation inside the pump. Our pumps are equipped with efficient cooling systems that ensure optimal performance even in high - humidity conditions.


In addition to the pump design and cooling system, proper maintenance is also crucial for ensuring the pump's ability to handle water vapor. Regularly checking the liquid level in the liquid ring pumps, monitoring the temperature, and replacing worn - out parts can go a long way in maintaining the pump's performance.
Let's take a look at some real - world examples. In a food processing plant, where steam is used for sterilization and cooking processes, there is a significant amount of water vapor in the air. A 2BE3 Large Liquid Ring Vacuum Pump can be used to create a vacuum environment for packaging and other processes. The pump's high - capacity design allows it to handle the large volumes of water vapor generated during these processes, ensuring a stable vacuum and efficient operation.
In a pharmaceutical manufacturing facility, where precise vacuum levels are required for processes like drying and distillation, a 2BED 2 Stage Liquid Ring Vacuum Pump can be used. The pump's ability to handle water vapor while maintaining a high vacuum level is essential for producing high - quality pharmaceutical products.
So, if you're in an industry that deals with water vapor and you need a reliable vacuum pump, we've got you covered. Our large vacuum pumps are designed to handle a wide range of water vapor loads, from moderate to extremely high. Whether you're a small business or a large - scale industrial operation, we have the right pump for your needs.
If you're interested in learning more about our products or want to discuss your specific requirements, don't hesitate to reach out. We're here to help you find the perfect vacuum pump solution for your application. Contact us today to start the conversation and let's work together to improve your vacuum system's performance.
References
- Vacuum Technology Handbook, various authors
- Industrial Vacuum Pump Applications, industry research reports