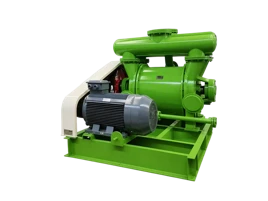
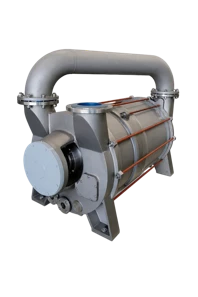
As a supplier of high flow vacuum pumps, I understand the importance of having readily available spare parts to ensure the continuous and efficient operation of these critical pieces of equipment. High flow vacuum pumps are used in a wide range of industries, including chemical processing, food and beverage, pharmaceuticals, and many others. In this blog post, I will discuss the commonly needed spare parts for high flow vacuum pumps and their significance in maintaining optimal performance.
Impellers
The impeller is one of the most crucial components of a high flow vacuum pump. It is responsible for creating the necessary centrifugal force to draw in and expel air or gas from the system. Over time, impellers can wear out due to friction, corrosion, or the presence of abrasive particles in the pumped medium. When an impeller becomes damaged or worn, it can lead to reduced pump efficiency, decreased flow rates, and increased energy consumption.
Replacing a worn impeller with a high - quality spare part is essential to restore the pump's performance. At our company, we offer a variety of impellers designed specifically for different models of high flow vacuum pumps, including the 2BED 2 Stage Liquid Ring Vacuum Pump, 2BE3 Large Liquid Ring Vacuum Pump, and 2BE1 Liquid Ring Vacuum Pump. These impellers are manufactured using high - grade materials to ensure durability and long - term performance.
Seals
Seals play a vital role in preventing leaks and maintaining the integrity of the vacuum pump system. There are different types of seals used in high flow vacuum pumps, such as mechanical seals and shaft seals. Mechanical seals are designed to prevent fluid leakage between the rotating shaft and the stationary pump housing. They consist of two flat surfaces that are held together by a spring, creating a tight seal.
Shaft seals, on the other hand, are used to prevent the ingress of air or the escape of the pumped medium along the shaft. Over time, seals can deteriorate due to chemical exposure, high temperatures, or mechanical wear. A damaged seal can lead to reduced vacuum levels, increased energy consumption, and potential contamination of the pumped medium.
We stock a comprehensive range of seals for high flow vacuum pumps. Our seals are made from high - quality materials that are resistant to chemicals, heat, and wear. By replacing worn seals promptly, you can ensure the reliable operation of your vacuum pump and avoid costly downtime.
Bearings
Bearings are essential components that support the rotating parts of the vacuum pump, such as the impeller and the shaft. They reduce friction and allow for smooth rotation, which is crucial for the efficient operation of the pump. There are different types of bearings used in high flow vacuum pumps, including ball bearings and roller bearings.
Ball bearings are commonly used in applications where high - speed rotation is required, while roller bearings are more suitable for heavy - load applications. Over time, bearings can wear out due to factors such as improper lubrication, excessive load, or contamination. Worn bearings can cause excessive vibration, noise, and even damage to other components of the pump.
As a supplier, we offer a wide selection of bearings for high flow vacuum pumps. Our bearings are sourced from reputable manufacturers and are designed to meet the specific requirements of different pump models. Regularly inspecting and replacing worn bearings can help extend the lifespan of your vacuum pump and improve its overall performance.


Gaskets
Gaskets are used to create a tight seal between different components of the vacuum pump, such as the pump housing, covers, and flanges. They prevent leaks and ensure the proper functioning of the pump. Gaskets are typically made from materials such as rubber, silicone, or graphite, depending on the application and the chemical compatibility requirements.
Over time, gaskets can become brittle, cracked, or deformed due to exposure to heat, chemicals, or mechanical stress. A damaged gasket can lead to air leaks, reduced vacuum levels, and potential contamination of the pumped medium. We provide a variety of gaskets for high flow vacuum pumps, including custom - made gaskets to fit specific pump models. By using high - quality gaskets and replacing them when necessary, you can maintain the integrity of your vacuum pump system.
Filters
Filters are an important part of the high flow vacuum pump system, as they help to remove contaminants from the pumped medium. There are different types of filters used in vacuum pumps, such as air filters, oil filters, and liquid filters. Air filters are used to prevent dust, dirt, and other particles from entering the pump, which can cause damage to the impeller, bearings, and other components.
Oil filters are used in oil - lubricated vacuum pumps to remove contaminants from the oil, ensuring proper lubrication and reducing wear on the moving parts. Liquid filters are used to remove solid particles from the liquid medium being pumped. Clogged filters can restrict the flow of the pumped medium, reduce pump efficiency, and increase energy consumption.
We offer a range of high - quality filters for high flow vacuum pumps. Our filters are designed to provide efficient filtration and long - term performance. Regularly replacing filters is an important part of vacuum pump maintenance, as it helps to ensure the reliable operation of the pump and extends its lifespan.
Check Valves
Check valves are used to control the flow of the pumped medium in one direction, preventing backflow. They are an important component in high flow vacuum pump systems, as they help to maintain the vacuum level and prevent damage to the pump caused by reverse flow. Check valves can be either mechanical or electronic, depending on the application.
Mechanical check valves operate based on the pressure difference between the inlet and the outlet, while electronic check valves are controlled by sensors and actuators. Over time, check valves can become stuck or damaged, which can lead to reduced vacuum levels and potential damage to the pump.
We supply a variety of check valves for high flow vacuum pumps. Our check valves are designed to provide reliable operation and long - term performance. Regularly inspecting and maintaining check valves can help ensure the proper functioning of your vacuum pump system.
Importance of Using Genuine Spare Parts
When it comes to replacing spare parts for your high flow vacuum pump, it is crucial to use genuine parts. Genuine spare parts are specifically designed and manufactured to meet the exact specifications of your pump model. They are made from high - quality materials and undergo rigorous quality control tests to ensure optimal performance and reliability.
Using non - genuine parts can lead to a variety of problems, including reduced pump efficiency, increased energy consumption, and potential damage to the pump. Non - genuine parts may not fit properly, which can cause leaks, vibration, and premature wear. Additionally, using non - genuine parts can void the manufacturer's warranty, leaving you responsible for any repair costs.
As a trusted supplier of high flow vacuum pumps and spare parts, we are committed to providing our customers with genuine spare parts that are of the highest quality. Our parts are sourced directly from the manufacturers, ensuring that you get the best - in - class products for your vacuum pump.
Conclusion
In conclusion, having a supply of commonly needed spare parts for your high flow vacuum pump is essential for ensuring its reliable and efficient operation. Impellers, seals, bearings, gaskets, filters, and check valves are some of the key components that may need to be replaced over time. By using genuine spare parts and performing regular maintenance, you can extend the lifespan of your vacuum pump, reduce downtime, and save on repair costs.
If you are in need of spare parts for your high flow vacuum pump or have any questions about our products, we encourage you to contact us. Our team of experts is ready to assist you in finding the right parts for your specific needs. We are dedicated to providing excellent customer service and ensuring that your vacuum pump operates at its best.
References
- "Vacuum Pump Handbook" by Klaus D. Timmerhaus and Ronald C. Reed
- "Industrial Vacuum Technology" by Peter K. Baumann